Reini R-series pumps
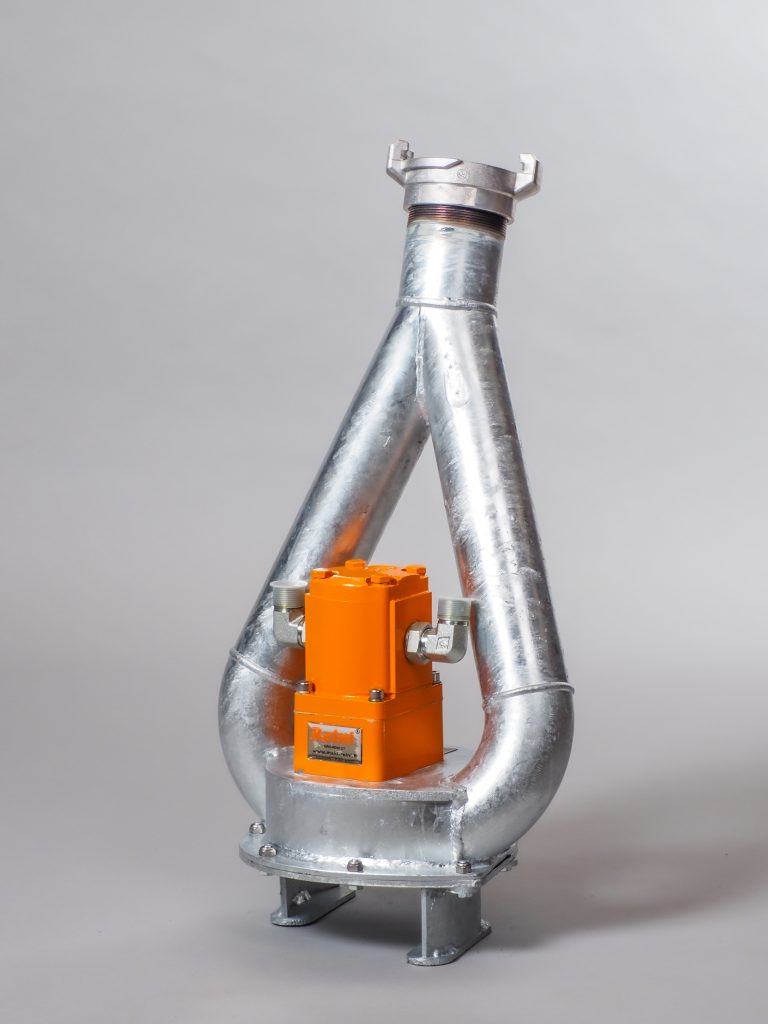
Reini-1R – Hydraulic Submersible Pump
The Reini-1R is a robust hydraulic submersible pump designed for versatile liquid handling applications.
It delivers a maximum flow of up to 3000 litres per minute, making it suitable for general water transfer, tank filling and intermediate dewatering tasks.
The pump is equipped with cutting blades at the suction inlet, which help break up softer material in the pumped media. This model is well suited for applications such as agricultural pit and well emptying, and civil engineering dewatering where pump size and mobility are key considerations.
Reini-1R features a quality gear motor drive and a greaseable support bearing for serviceability. Typical operating limits include a maximum lift of 35 m, hydraulic flow up to 50 l/min, and hydraulic pressure up to 250 bar.
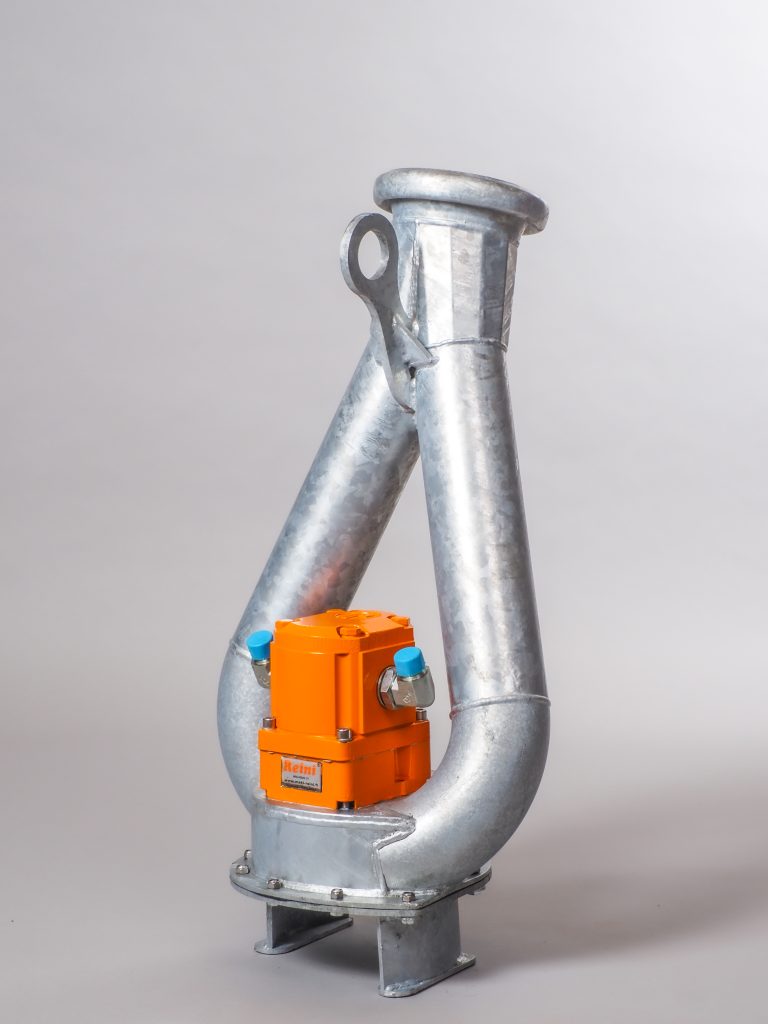
Reini-2R – Hydraulic Submersible Pump
The Reini-2R is a versatile hydraulic submersible pump suited for a wide range of liquid transfer and slurry handling tasks.
It delivers a maximum flow of up to 5000 litres per minute and is commonly used on construction sites, in agriculture and for loading slurry tankers thanks to its strong overall capacity and robust design.
Powered by the hydraulic system of a tractor, excavator or similar machinery, the 2R uses a high-quality gear motor drive with a greasable support bearing that enhances serviceability and durability in extended use.
Typical operating capabilities include a maximum lifting height of 30 m, a permitted hydraulic flow up to 100 l/min and hydraulic pressure up to 250 bar. The pump’s rugged build and ease of installation make it suitable for general water handling, slurry transfer and other demanding field applications.
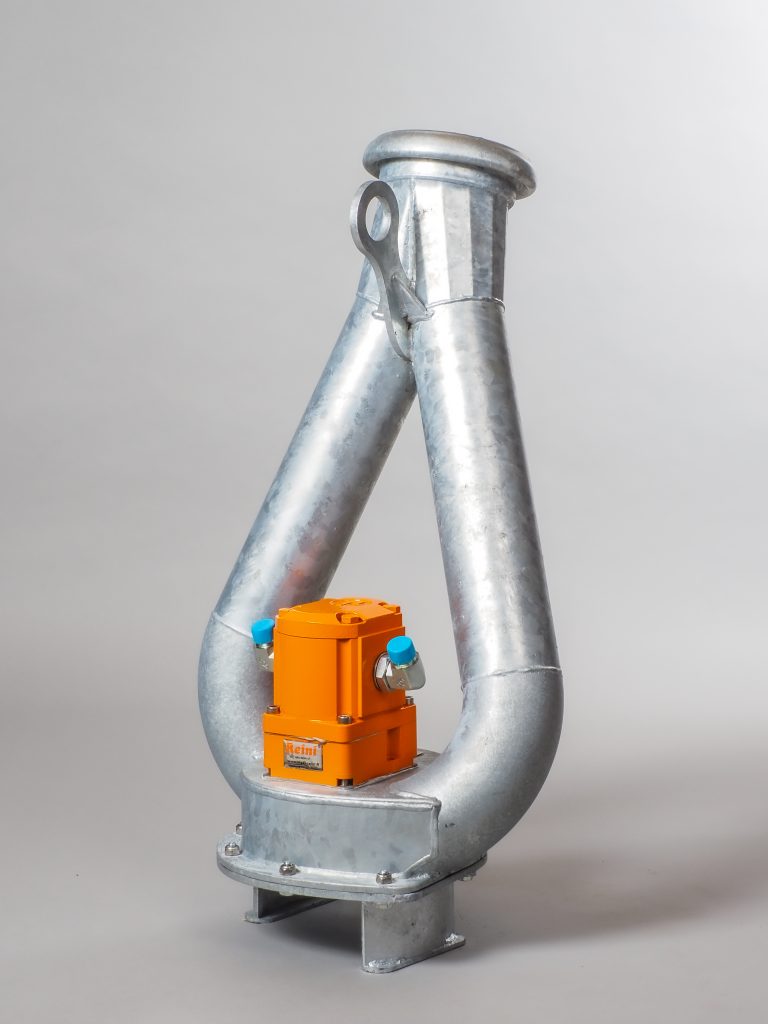
Reini-3R – Hydraulic Submersible Pump
The Reini-3R is a compact hydraulic submersible pump engineered for demanding slurry and liquid transfer applications.
It delivers a maximum flow of up to 6000 litres per minute, making it suitable for more substantial slurry handling and general transfer tasks where greater output is needed compared to smaller R-series models.
The 3R model is designed with features that support reliable operation in field conditions, including a greasable support bearing that protects the pump drive from excessive loads and contamination, and a tangle protection in the pump housing to reduce the risk of material wrapping around the impeller shaft.
With typical hydraulic limits up to 100 l/min flow and 250 bar pressure, the Reini-3R is commonly used on tractors and similar mobile machinery where robust performance and simplicity are required.